Choosing pcb fabrication and assembly is not merely a purchasing decision. It is a way to control design accuracy, production consistency, and product risk. A capable partner connects engineering files with real factory processes. This includes material selection, impedance control, stencil design, component placement, soldering, inspection, and final testing. Each step matters. A misplaced 0201 resistor can stop an otherwise excellent product.
Tara Dunn, a recognized PCB industry educator and president of Omni PCB, has said, “The key to successful PCB design is understanding the capabilities and limitations of the fabricator.” Her point is practical. Early communication can prevent costly redesigns, weak solder joints, delayed prototypes, and unexpected yield problems. Experienced providers also use documented procedures, trained technicians, supplier controls, and traceability records. These details support dependable results under IPC-based quality expectations.
Still, outsourcing is not automatically safer. The wrong supplier may offer an attractive price while hiding unclear tolerances or weak inspection practices. Some teams also assume assembly begins after fabrication, but the two stages influence each other from the start. A practical evaluation should examine sample boards, factory equipment, testing methods, engineering support, and delivery history. Ask difficult questions.
Good pcb fabrication and assembly services should make problems visible before volume production. They should explain limitations without exaggeration. Perfect results are never guaranteed, and that deserves honest attention. However, a transparent partner can reduce uncertainty with design-for-manufacturing reviews, prototype testing, automated optical inspection, and functional checks. That combination helps engineers move from a digital layout to a reliable, tested product.
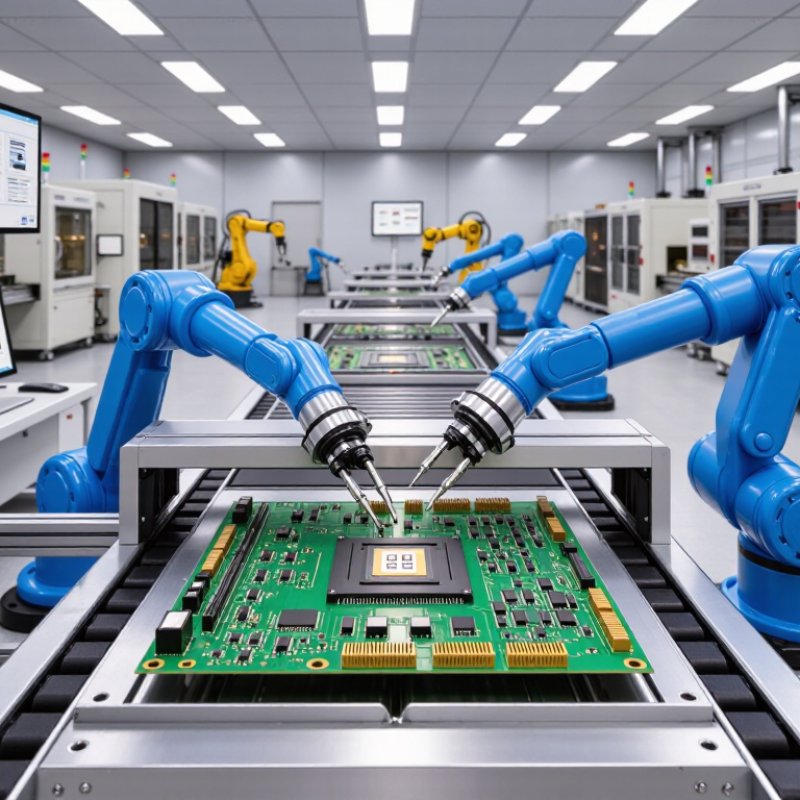
PCB fabrication and assembly are two linked stages in PCB production. Fabrication creates the board’s physical structure. Assembly places components onto that structure and turns it into a working circuit. Treating them separately can create avoidable delays, especially when pad layouts, tolerances, or material choices do not match.
Prismark’s 2024 market update estimated global PCB sales at roughly US$69 billion in 2023. It also forecast renewed industry growth as demand rises for automotive, industrial, and communication electronics. These figures show why controlled production matters. A fabrication team must review layer counts, copper thickness, drilling, impedance, and surface finish. An assembly team then checks component footprints, solder paste openings, placement accuracy, and thermal profiles. Small mismatches can become expensive rework.
The link is practical. A fabrication engineer may adjust a via design before assembly problems appear. An assembly technician may report solder bridging near fine-pitch pads. Useful feedback travels backward. It should. IPC process guidance and acceptance standards help teams define measurable quality requirements, while inspection data supports traceability. Automated optical inspection can detect missing or shifted components, but it cannot replace careful design review. The process is not flawless. A clean prototype may still reveal heat imbalance during production. That lesson should change the next revision. Careful coordination reduces handling, shortens communication paths, and gives engineers clearer responsibility for each board.
One ounce of copper means 1 oz per square foot, or about 35 μm before processing. It is not a finished-board guarantee. Etching reduces width, while plating may increase selected areas. That difference affects impedance and current capacity. IPC-2221 and IPC-2152 provide useful design guidance for conductor spacing and thermal performance. Still, calculations need real stackup data.
Material selection begins with operating frequency, temperature, and voltage. Standard epoxy laminate suits many digital boards, but high-speed links may require controlled dielectric properties. A 2024 IPC technology roadmap repeatedly identified signal integrity and thermal management as major design pressures.
Copper also matters commercially. The U.S. Geological Survey reported approximately 22 million metric tons of mined copper production worldwide in 2023. Prices can change quickly. A thicker layer is not automatically safer.
Finish selection should match assembly conditions and storage time. Organic coating can control cost, while immersion metal finishes support fine-pitch soldering. Hot-air leveling may leave uneven surfaces.
Small detail, large consequence.
In fabrication reviews, I often see designers specify “1 oz” without defining finished copper, dielectric thickness, or roughness. That shortcut is tempting, but incomplete. IPC-6012 acceptance requirements help convert those assumptions into measurable criteria.
The honest question is not only, “Can this board be built?” It is, “Will the finished stackup remain stable after fabrication, assembly, and field use?”
Why Choose PCB Fabrication and Assembly Services?
IPC-A-600 defines the acceptability of bare printed boards. IPC-A-610 evaluates completed electronic assemblies. Together, they turn quality into visible, measurable conditions. Inspectors check conductor width, annular rings, laminate damage, solder coverage, component placement, and contamination.
Details matter. A weak solder joint may look acceptable under ordinary lighting. Under magnification, insufficient wetting or a fractured fillet can appear. IPC-A-610 provides clearer acceptance criteria for these defects. IPC’s 2024 Electronics Industry Sentiment Survey reported that 65% of respondents expected sales growth, while skilled-labor shortages remained a major operational concern. That pressure makes repeatable inspection increasingly valuable.
Experienced fabrication and assembly teams use controlled work instructions, lot records, and inspection photographs. They also match the acceptance class to the product’s risk. Class 2 may suit general electronics, while Class 3 demands stricter evidence for high-reliability applications. IPC-A-600 and IPC-A-610 support this discipline, but they do not replace engineering judgment. No standard removes every failure.
A practical review should compare first-article results with the drawing, materials, and customer requirements. The uncomfortable truth is that “pass” can still hide weak process control. IPC’s 2023 Global Electronics Manufacturing Survey also identified supply-chain instability and workforce capability as continuing industry challenges. Reliable service requires documented corrections, not optimistic assumptions.
| Quality Dimension | IPC-A-600: Printed Board Acceptability | IPC-A-610: Electronic Assembly Acceptability | Value of Professional Fabrication and Assembly |
|---|---|---|---|
| Primary scope | Covers the acceptability of fabricated printed circuit boards before components are installed. | Covers the acceptability of assembled electronic products, including component mounting, soldering, and workmanship. | Connects bare-board quality with assembly quality through a controlled, documented production process. |
| Quality classes | Uses Classes 1, 2, and 3 to represent increasing levels of product performance and reliability expectations. | Uses Classes 1, 2, and 3 for general, dedicated-service, and high-reliability applications respectively. | Allows inspection depth and acceptance criteria to match the product’s operating environment and risk level. |
| Copper features | Evaluates conductor definition, etching, spacing, surface condition, and visible defects that may affect function. | Checks whether exposed pads, lands, and conductors remain suitable for soldering and electrical connection. | Process controls help reduce open circuits, shorts, insufficient clearances, and damaged solderable surfaces. |
| Plating and surface finish | Addresses the condition and coverage of plated features and the suitability of the board surface for its intended use. | Considers whether component connection areas support acceptable solder joints and reliable assembly workmanship. | Material selection and incoming inspection can improve solderability, consistency, and long-term connection reliability. |
| Holes and vias | Reviews hole quality, registration, annular features, plating continuity, and conditions that could compromise interconnection. | Checks component-hole soldering, lead insertion, solder coverage, and visible evidence of acceptable connections. | Fabrication inspection and assembly inspection address both the internal interconnect and the finished solder joint. |
| Lamination and board structure | Includes visible conditions such as delamination, measling, blisters, warpage, and other structural concerns, subject to applicable requirements. | Focuses on the assembled board and does not replace fabrication-level evaluation of internal laminate integrity. | Using both standards helps prevent a structurally unsuitable board from reaching the assembly stage. |
| Component placement | Not the primary focus because the standard applies to unassembled printed boards. | Evaluates component presence, orientation, polarity, alignment, seating, clearance, and lead condition. | Automated placement equipment, programming controls, and visual inspection improve repeatability and traceability. |
| Solder joints | Evaluates the board features that provide the foundation for soldering, such as pads, lands, and plated holes. | Defines visual acceptability for solder conditions, including wetting, coverage, bridges, void-related concerns where applicable, and other joint characteristics. | Controlled solder profiles and inspection help reduce rework, latent defects, and inconsistent electrical connections. |
| Cleanliness and residues | Addresses board condition and visible contamination in relation to the specified manufacturing requirements. | Considers residues, foreign material, and cleanliness conditions that may affect assembly performance or reliability. | Cleaning controls, process monitoring, and verification can lower contamination-related failure risks. |
| Inspection approach | Primarily supports visual evaluation of fabricated boards, supplemented by engineering and test requirements when specified. | Primarily supports visual evaluation of assemblies; additional inspection or testing may be required by the product specification. | Combining visual inspection with electrical, dimensional, or automated inspection creates stronger process evidence. |
| Documentation required | Acceptance depends on the applicable drawing, material requirements, board construction, and agreed product class. | Acceptance depends on the assembly drawing, component data, workmanship requirements, product class, and customer-defined exceptions. | Clear specifications reduce interpretation differences and make nonconformance decisions more consistent. |
| Typical quality records | May include material certifications, dimensional reports, inspection results, and electrical test records when specified. | May include component traceability, inspection results, rework records, process data, and functional test results when specified. | A documented chain of evidence supports troubleshooting, corrective action, and production repeatability. |
| Best use in a project | Use when defining and reviewing the quality of the bare PCB before assembly. | Use when defining and reviewing the quality of the populated and soldered PCB assembly. | Using both standards provides a more complete quality framework from board production through finished assembly. |
| Important limitation | It is an acceptability standard and does not by itself define every design, material, performance, or reliability requirement. | It is an acceptability standard and does not replace the product design, process specification, testing plan, or customer requirements. | Project documentation should identify the applicable revision, product class, acceptance criteria, and any documented exceptions. |
Note: Acceptance criteria should be agreed with the design authority and applied according to the applicable IPC standard revision, product class, drawings, and purchase specifications.
Why Choose PCB Fabrication and Assembly Services?
4 mm-Pitch SMT: Increasing Circuit Density and Placement Accuracy
Surface-mount technology can reduce board size while improving placement consistency. However, the term 4 mm pitch needs careful review. In common SMT engineering, 0.4 mm pitch is considered fine-pitch, while 4 mm pitch is relatively wide. A 0.4 mm grid offers 100 times more theoretical placement density than a 4 mm grid, based on center-to-center area.
That difference affects routing, solder paste design, and component selection. At fine pitch, a small stencil offset can create bridging or insufficient solder joints. Automated optical inspection and X-ray inspection help identify these defects before shipment. IPC workmanship requirements also emphasize pad geometry, solder coverage, and process control rather than placement speed alone. Precision must be measured.
A 2024 market outlook from Fortune Business Insights valued the global SMT equipment market at approximately 4.3 billion dollars in 2023. It projects nearly 6.9 billion dollars by 2030, showing continued investment in automated assembly. Yet equipment alone cannot guarantee reliable boards. Fabricators must control feeder calibration, fiducial recognition, humidity, and reflow profiles. The Global Electronics Association’s industry surveys also continue to highlight supply-chain pressure and manufacturing capacity concerns. In practice, a stable process often matters more than an impressive placement specification. Some assumptions deserve checking.
Smaller SMT pitches allow more theoretical component positions within the same PCB length. The density values are calculated as 100 mm divided by pad pitch, while the placement-tolerance values represent practical engineering targets for modern automated SMT assembly. Actual results depend on the component package, PCB design rules, solder paste process and inspection capability.
Why Choose PCB Fabrication and Assembly Services?
DFM begins before the first board is etched. Engineers review clearances, drill sizes, thermal reliefs, and component footprints. These checks reduce fabrication surprises and assembly delays. IPC-2221 design guidance supports this discipline through defined spacing and layout practices. Yet, DFM is not flawless. A library footprint can still carry an outdated dimension. Small misses matter.
AOI checks solder joints, polarity, placement, and visible component defects. It can detect a shifted resistor beside a fine-pitch package within seconds. X-ray inspection examines hidden joints, vias, voids, and package connections. This matters for bottom-terminated components and dense multilayer boards. NIST Planning Report 00-02 estimates poor quality can cost 15–20% of sales across many industries. Rework also adds handling, labor, heat exposure, and schedule risk. IPC-A-610 provides widely used acceptance criteria, but inspection cannot replace process control. A clean image may still hide a weak process.
Tips: Send the complete bill of materials and fabrication files early. Mark critical nets and high-risk packages. Set AOI limits with approved samples, not assumptions. Use X-ray on hidden joints and new package types. Record recurring defects by location and cause. That data improves the next DFM review. An experienced fabrication and assembly partner can connect these findings across design, production, and inspection.