2026 How to Choose the Best Cut And Die Machine?
Choosing the right Cut And Die Machine in 2026 requires more than comparing speed and price. The best choice depends on your materials, production volume, cutting accuracy, and finishing requirements. A machine for adhesive labels may not suit thick carton, foam, leather, or layered film. Small details matter.
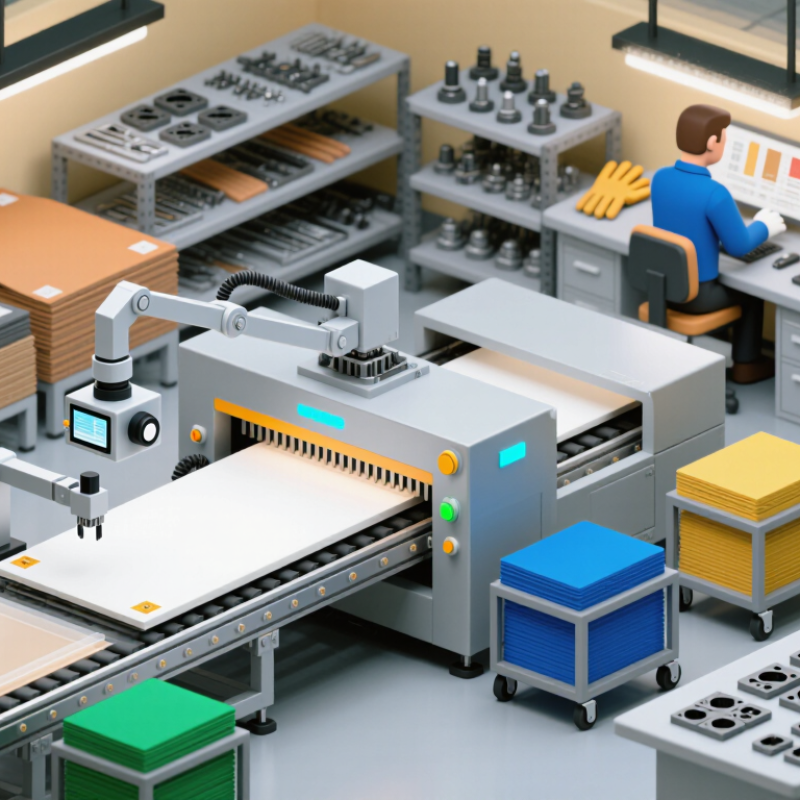
Picture a busy production floor. Sheets enter the feeder, registration marks align under a camera, and the die presses cleanly through each layer. If alignment shifts by even one millimeter, waste can increase quickly. Buyers should examine maximum sheet size, cutting pressure, tooling compatibility, automation, noise, and changeover time. They should also ask about operator training, spare parts, software updates, and local technical support. These practical factors often matter more than impressive brochure figures.
No machine is perfect. A faster model may create more setup challenges. A lower-priced model may bring higher maintenance costs later. Even experienced buyers can overlook material testing before purchase. Requesting samples and testing the actual substrate can reveal problems early. Reliable manufacturers should provide clear specifications, safety documentation, service records, and realistic performance data. Independent reviews and feedback from comparable businesses can strengthen the decision.
This guide explains how to compare machine types, evaluate essential features, estimate total ownership costs, and avoid common purchasing mistakes. It also considers energy use, waste reduction, operator safety, and future production changes. The goal is not to select the most advanced machine. It is to find the most dependable fit for your real workflow.
Define Machine Types, Materials, and 2026 Production Requirements
2026 How to Choose the Best Cut And Die Machine?
Define Machine Types, Materials, and 2026 Production Requirements
Choosing a cut and die machine starts with the material, not the machine catalog. Flatbed systems suit short runs, prototypes, and thick paperboard. Rotary machines deliver speed for continuous label and packaging production. Digital cutters work well when designs change frequently. In real production trials, setup time often matters more than maximum cutting speed. A fast machine can still lose hours during tool changes.
List every material you plan to process. Include paper, corrugated board, foam, film, adhesive sheets, and laminated stock. Record thickness, surface finish, stiffness, and cutting tolerance. Materials can behave differently after humidity changes. That detail is easy to miss. Ask for sample testing with your actual files and materials. Inspect edges, waste removal, registration, and tool marks under normal lighting.
Your 2026 requirements should include output targets, automation, energy use, operator safety, and digital workflow compatibility. Check automatic feeding, camera registration, quick-change tooling, and production data collection. A practical tolerance is more valuable than an impressive brochure number. Calculate payback using real orders, not hopeful forecasts. Leave room for future materials and smaller batch sizes. I have seen buyers overestimate demand and purchase excessive capacity. That mistake can make maintenance and training unnecessarily expensive.
Compare Press Force, Cutting Speed, and ±0.01 mm Registration Accuracy
Choosing a cut and die machine starts with the material, not the advertised maximum. Press force determines whether sheets cut cleanly without crushed edges or incomplete corners. Thick board, laminated film, and layered labels require different force reserves. A machine operating near its limit may produce inconsistent results. Leave practical headroom. Too much force, however, can increase tool wear and energy use. Ask for measured force data under your material conditions, not only a catalog figure.
Cutting speed affects output, but speed alone does not define productivity. A slower stroke with stable feeding can outperform a faster machine that creates rejects. Watch acceleration, dwell time, and changeover time during a trial. Registration accuracy matters when printed graphics meet die lines. A claimed ±0.01 mm tolerance sounds precise. It may apply only to controlled samples, clean tooling, and ideal temperatures. Confirm repeatability across a full sheet, several cycles, and normal operator adjustments. Use registration marks, calibrated vision sensors, and a documented measurement method. Tiny offsets become obvious around narrow borders.
In practical trials, compare three samples: a simple shape, fine detail, and a multi-layer job. Record force, speed, waste, noise, and setup minutes. Do not ignore maintenance access. Dust on sensors can quietly reduce alignment accuracy. Test results may weaken after long runs. That is worth questioning. Select the machine whose verified performance matches your materials, operators, and quality tolerance.
Match Die Formats and Working Areas to 0.1–2.0 mm Material Thickness
2026 How to Choose the Best Cut And Die Machine?
Material thickness changes the machine decision. A 0.1 mm film behaves differently from a 2.0 mm board. Thin films may stretch, curl, or cling during feeding. Thicker sheets need greater cutting force and stable pressure control. Do not judge capacity by thickness alone. Material hardness, surface coating, grain direction, and compressibility also affect results.
Match the die format to the working area. A flatbed die suits frequent format changes and precise short runs. Rotary formats can support faster continuous production when dimensions remain consistent. The working area should cover the finished part, waste margin, registration marks, and safe clamping space. A die that barely fits may create uneven pressure near its edges. Allow practical clearance.
Test real samples.
For 0.1–0.3 mm materials, inspect feeding tension and edge curling after cutting. From 0.3–1.0 mm, check whether the machine maintains clean cuts across the full bed. At 1.0–2.0 mm, examine pressure stability, board compression, and stripping performance. Measure ten pieces, not one. Small errors often appear only after repeated cycles. I have found that a neat specification sheet can still mislead when humidity changes the material. Leave room for adjustment. The ideal machine is not merely the strongest one; it is the model that maintains accuracy across your actual formats, tools, and production speed.
2026 How to Choose the Best Cut and Die Machine?
Match die formats and working areas to material thickness from 0.1–2.0 mm.
This reference chart matches common nominal die formats with material-thickness ranges. Larger working areas improve sheet utilization, while thinner materials generally support smaller and faster die formats. Actual machine selection should also consider material hardness, tensile strength, cutting force, feed accuracy, and required production speed.
Evaluate Servo Automation, Safety Standards, and 60–120 Strokes per Minute
2026 How to Choose the Best Cut And Die Machine?
A practical evaluation starts with the servo system, not the advertised speed. Servo automation can control feeding, positioning, and die movement with consistent timing. This reduces setup errors and supports repeatable results across long production runs. Ask for data at your actual material thickness and cutting pattern. Speed is not everything.
A useful working range is 60–120 strokes per minute. Lower speeds may suit thick, delicate, or difficult materials. Higher speeds can improve output, but only when feeding remains stable and waste stays controlled. During a factory trial, inspect cut edges, registration accuracy, vibration, noise, and temperature. Watch the waste. A machine that runs quickly but creates frequent jams may cost more in labor and downtime.
Safety must be checked as carefully as productivity. Look for fixed guards, interlocked access doors, emergency stops, safe maintenance modes, and clear operator controls. The machine should support a documented risk assessment and comply with applicable regional safety standards. Request manuals, inspection records, and training procedures before purchase. Operators should understand lockout procedures and safe die changes. These details are often treated as paperwork, yet they shape daily reliability. I have seen evaluations focus heavily on stroke rate while overlooking changeover access. That was a mistake. A short trial cannot reveal every maintenance problem, so leave room for further verification.
Calculate Energy Use, Maintenance Costs, and Five-Year ROI
How to Choose the Best Cut and Die Machine in 2026
A low purchase price can hide expensive energy and maintenance demands. The U.S. Department of Energy reports that motor-driven systems use about 69% of industrial electricity. Measure real consumption instead of trusting the nameplate.
For example, a 7.5 kW machine running 1,600 hours yearly at 80% load uses 9,600 kWh. At $0.12 per kWh, energy costs reach $1,152 annually. Over five years, that becomes $5,760 before tariff changes.
Add blades, dies, lubrication, calibration, labor, and downtime.
Build a five-year ROI model with three lines: energy, maintenance, and production value. A machine costing $35,000 may save $4,000 yearly through lower power use and fewer stoppages.
Its simple five-year return equals ($20,000 minus service costs) divided by the purchase price.
My first calculation was too optimistic because it ignored setup waste and weekend standby power. That mistake matters. Deloitte’s predictive-maintenance research indicates potential maintenance-cost reductions of 10% to 40%, but actual results depend on data quality and operator discipline.
Treat published ranges as planning references, not promises.
Tips
Install a temporary power meter for two production weeks.
Record idle, cutting, and die-adjustment loads separately.
Request maintenance records for similar machines.
Ask about spare-part lead times and technician training.
Include inflation, electricity-rate changes, and one unexpected repair in the model.
A spreadsheet that survives these assumptions is more useful than a polished sales estimate.